011
CNC aluminum enclosures
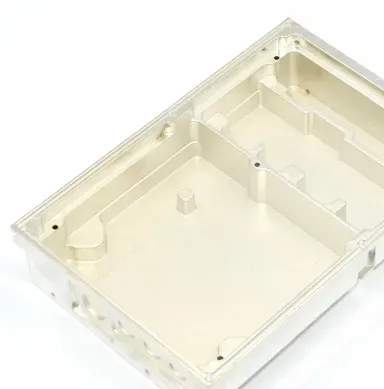
instrument cases, controller housings, equipment chassis and covers machined from 6061 or 6063, with connector cutouts, display windows and threaded inserts' holes machined to the drawing
INDUSTRIES
Enclosures rarely fail on the headline spec. They fail on the lid that rocks on its gasket because the mating face is not flat. On an anodized batch that comes back a shade off the last one.
On fins too thin to survive machining, or a button that suddenly needs a second supplier because nobody thought about the two-color step until the housing was done.
CNC machining, anodizing and other finishes, tooling and molding under one roof — so one factory answers for the enclosure, its finish and the parts that fit into it.
STEP, STP, IGES, STL, X_T and 2D PDF accepted. All files confidential; NDAs welcome.
instrument cases, controller housings, equipment chassis and covers machined from 6061 or 6063, with connector cutouts, display windows and threaded inserts' holes machined to the drawing
finned heatsinks machined from solid or to your extrusion profile, thermal interface plates and cold plates where flatness decides performance
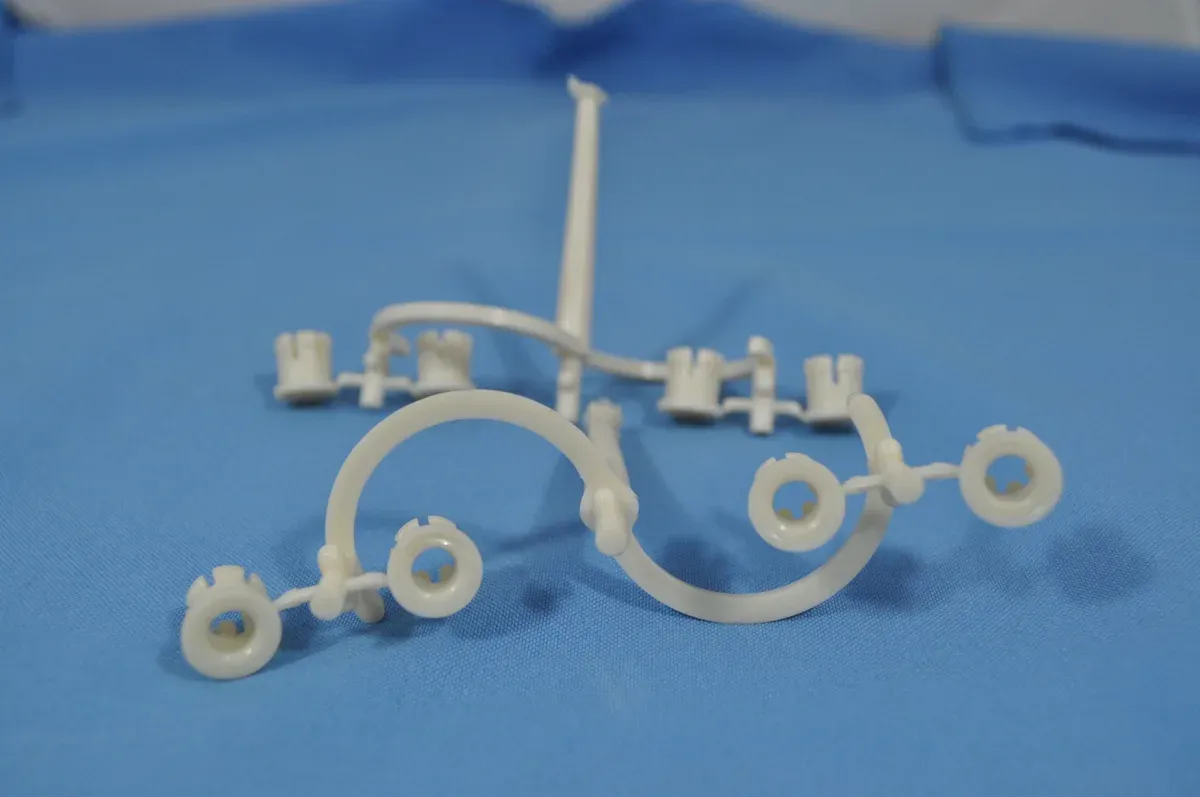
injection molded enclosures, front panels and internal chassis parts in ABS, PC and PC blends, from tools we build in-house
molded-in legends and color zones, soft-touch overmolded grips and seals
brackets, standoffs, shielding cans' frames and mounting plates in aluminum, brass and stainless
POM gears, insulators, spacers and wear parts, machined or molded depending on volume
An enclosure is flat things that have to meet. We hold precision tolerances (±0.025 mm / ±0.001 in) on the faces and hole patterns you mark, keep the rest at standard ISO 2768-mK (±0.13 mm), and inspect on CMMs. Lids close. Gaskets compress evenly. Boards mount without persuasion.
Color and texture drift when anodizing is an afterthought, outsourced after machining. Here machining and finishing sit in one order — bead blasting before anodizing for a uniform matte base, clear or colored anodizing, hardcoat where wear matters —
and the same factory answers for the finished dimensions, build-up included. Note it on the drawing and we machine with the allowance in mind.
Tall, thin fins and deep narrow slots are the classic heatsink cost trap. The free DFM review flags the fin ratios and pocket depths that will slow machining drastically,
then suggests the smallest change that leaves your thermal design intact — often a slightly wider slot, or splitting the part into a base plate plus a finned insert.
One vendor machines the shell, another molds the internals, a third does the buttons — and every interface problem belongs to nobody. We machine the metal, build the mold and mold the plastic in one building.
Shell, internal housing and two-color buttons can ship as one order, with one factory to call.
An enclosure gives the product away. Every file is treated as confidential by default, and NDAs are welcome before you send anything — ask, and we sign first.
6061 for general enclosures, 6063 where anodizing appearance leads, 7075 where the housing is also structure; brass and copper for terminals and thermal parts;
stainless for fittings and shafts. Maximum part size within 800 mm (31.5 in) CNC travel; MOQ 1 piece.
bead blasting, clear and colored anodizing, hardcoat anodizing, brushing, polishing, painting and powder coating, plating (nickel, chrome, zinc) and electroless nickel. Tell us the cosmetic standard the part must match; visible surfaces are quoted and inspected as cosmetic surfaces.
ABS for general housings, PC for impact resistance and transparent covers, POM for gears and sliding parts, PA where toughness and heat meet. Transparent and cosmetic parts run from in-house polished cavities.
POM, PC, ABS, PA, PEEK, PTFE and UHMW machined for low-volume electrical parts, insulators and fixtures, to the plastic tolerance levels of ISO 2768-mK (±0.25 mm standard, ±0.05 mm precision on suitable dimensions).
TOLERANCES AND QUALITY CONTROL
For enclosures the pattern is usually simple: precision ±0.025 mm on mating faces, connector cutout positions and board-mounting hole patterns; standard everywhere else.
you see the cost logic up front, not buried in a unit price.
Reports available: CMM and dimensional reports, material certificates, surface finish certificates, FAI reports, and pre-shipment photos or video — useful when the person approving the first article is on another continent.
Scope: Manufacturing of Hardware Molds and Parts. Full details: Quality & Inspection. The machines: Our Factory & Equipment.
3D model, 2D drawing with tolerances, finish and color requirements, quantity. NDAs welcome.
including fin/pocket manufacturability notes and a finish recommendation where relevant.
machined parts or T1 samples from the production tool, shipped with reports on request for your approval.
machining, anodizing and molding completed in-house as one order.
DDP, EXW or FOB to the US, Germany, France, Portugal, Sweden, Spain and beyond. Payment by T/T.
Precision Aluminum CNC Machined Parts · Custom Injection Molded Parts · Materials hub: Aluminum · Guide: How to Get an Accurate CNC Machining Quote
Upload the model — the free DFM review checks the mating faces, the fins and the finish before you commit, with a quote within 24 hours. Get a Quote — Contact Us.