CNC Machined Parts
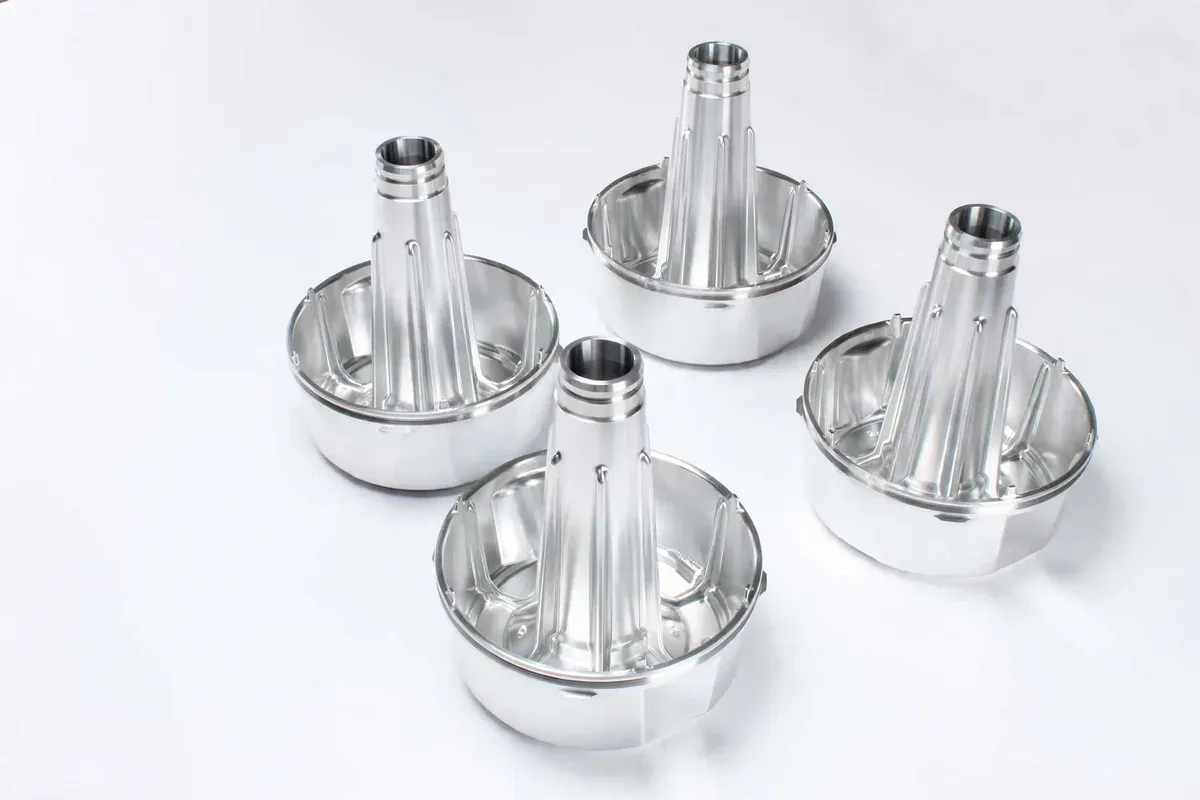
Precision Aluminum CNC Machined Parts
Precision aluminum parts CNC machined in-house from 6061, 7075, 6063 and 6082 — milled on 3, 4 and 5-axis centers, tolerances to ±0.025 mm, anodizing and other finishes in one order. No MOQ: 1-piece prototypes to production runs, free DFM and a quote within 24 hours.
Aluminum is usually the first material engineers reach for — light, strong enough for most structural jobs, and fast to machine. The problem is rarely the metal. It is the supplier: quotes that take a week, tolerances that drift between the prototype and the production batch, and anodizing sent to a second vendor who answers to nobody. At HAFO Mould, aluminum parts are machined, inspected and finished under one roof in Dongguan, China — in the same factory since 2007. Send a STEP file and an engineer reviews it free, with a quote back within 24 hours.
Upload Your Drawing — Free DFM + Quote Within 24 Hours. We accept STEP, STP, IGES, STL, X_T and 2D PDF drawings. All files are treated as confidential; NDAs are welcome.
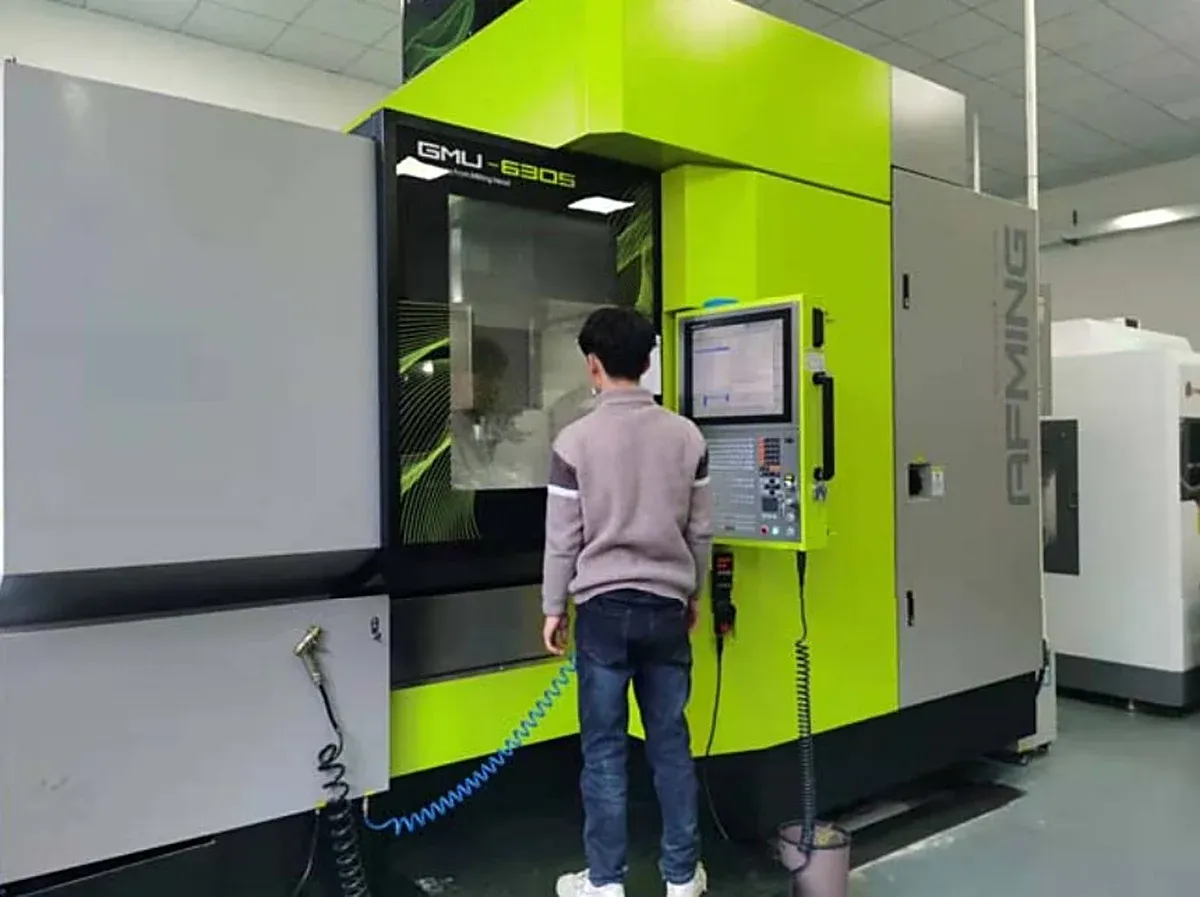
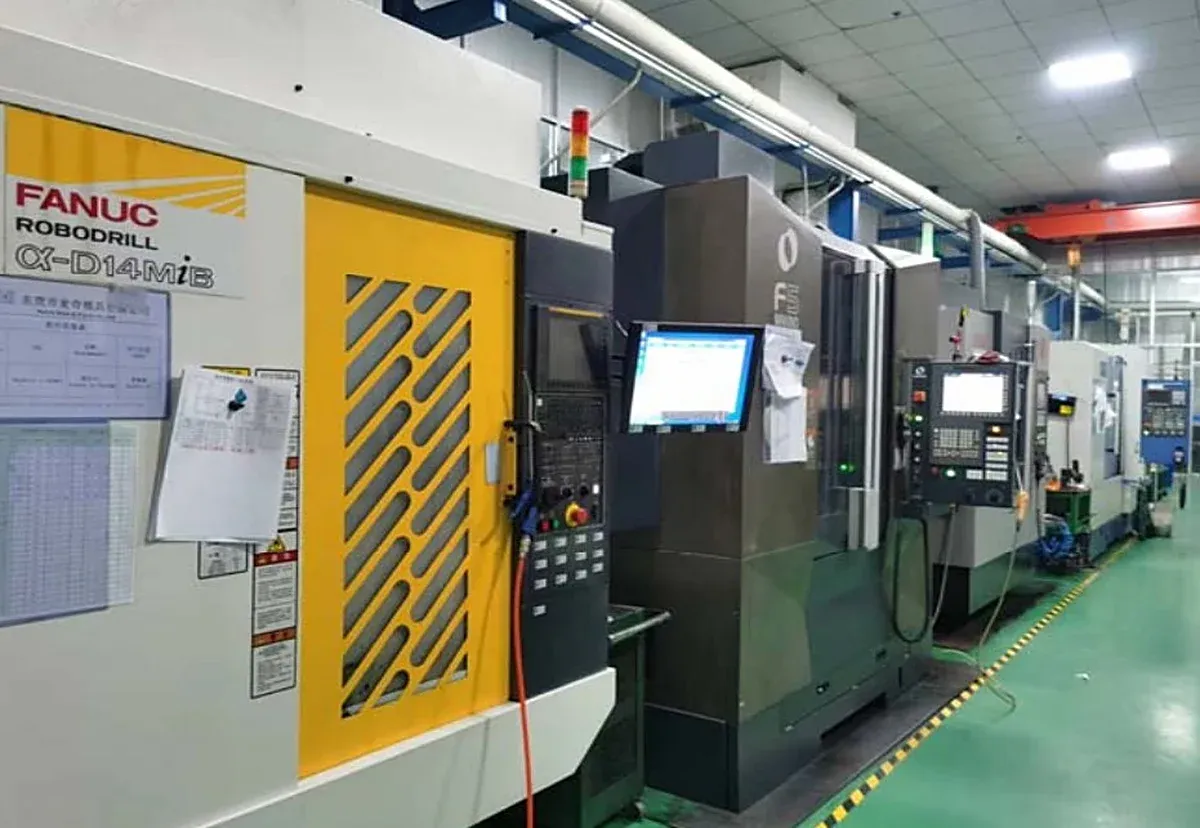
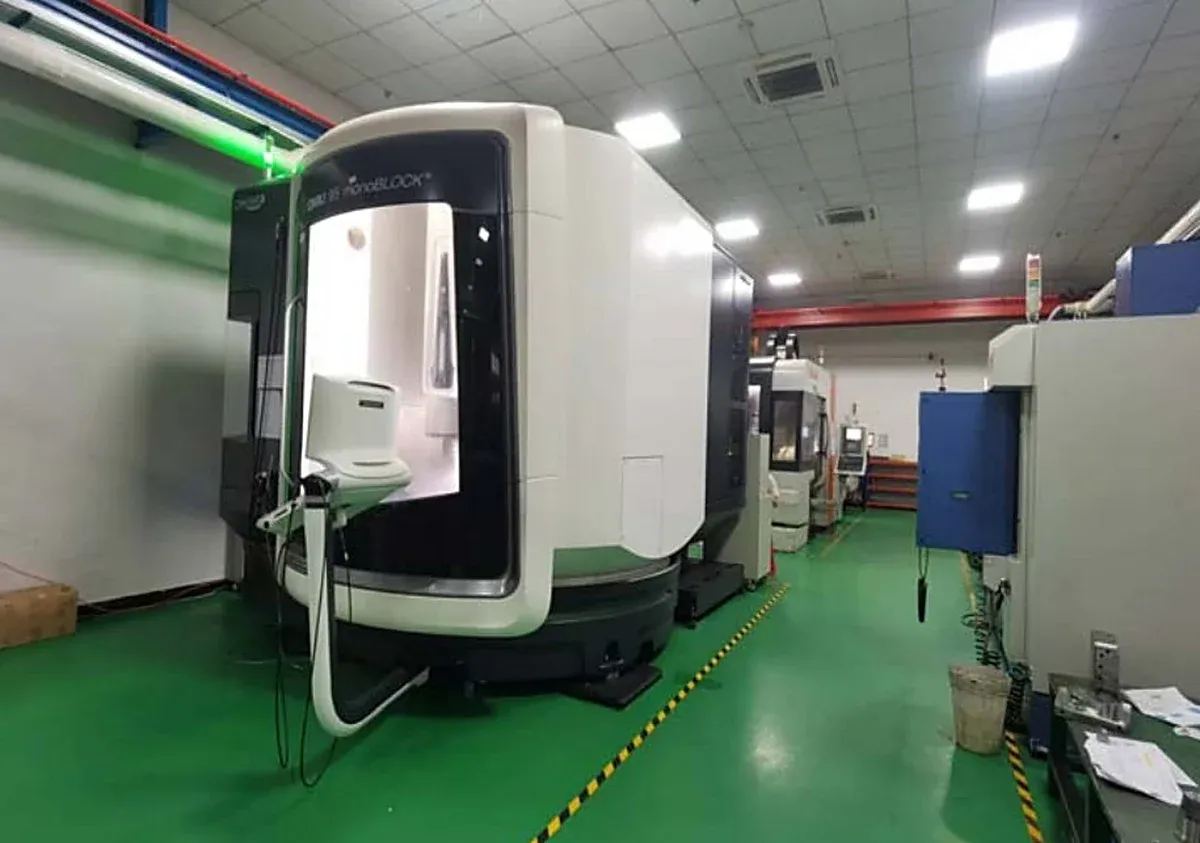
Since 2007 · 5,000 m² factory · 123 staff, 35 engineers · 69 CNC machining centers (38× 3-axis, 13× 4-axis, 18× 5-axis) · 3 fully automatic CMMs · ISO 9001:2015 certified — scope: Manufacturing of Hardware Molds and Parts · Parts shipped to customers worldwide.
What We Machine in Aluminum
- Enclosures and housings — electronics cases, instrument housings and covers with tight flatness on mating faces
- Brackets and structural parts — mounting brackets, frames, arms and supports where weight matters
- Plates and panels — base plates, front panels, heat-sink plates with drilled and tapped hole patterns
- Heat sinks and thermal parts — finned profiles machined to your extrusion or from solid
- Complex 5-axis parts — curved surfaces, angled features and undercuts machined in one setup on our 18 five-axis centers
- Prototypes and bridge parts — 1-piece and small-batch parts that later move into CNC Machined Parts production or into tooling
Machining Capabilities
Our 69 machining centers cover the full range of aluminum work, from simple 3-axis plates to multi-surface 5-axis components. Maximum CNC travel is 800 mm (31.5 in), which covers the large majority of aluminum enclosures, plates and housings. Turning and mill-turn work is handled in-house as well, so a part that needs both a turned bore and milled features does not change suppliers halfway through. Wire EDM and EDM are available in the same factory for sharp internal corners and features a rotating cutter cannot reach.
Every aluminum job starts with a free DFM (design for manufacturability) review. An engineer — not a salesperson — checks wall thicknesses, internal radii, deep pockets, hole depths and tolerance callouts, and flags anything that will add cost or risk before we quote. If a precision tolerance is marked on a face that does not need it, we will tell you, because that is where most avoidable machining cost hides.
Aluminum Grades We Machine
- 6061 — the general-purpose choice: good strength, excellent machinability, weldable, and the most economical option for most brackets, plates and housings
- 7075 — high-strength alloy for parts that carry real loads; often chosen where a steel part is being redesigned in aluminum
- 6063 — smooth surface and good anodizing response; common for enclosures, trims and parts where appearance matters
- 6082 — strong structural alloy widely specified on European drawings
Not sure which grade your part needs? Send the drawing and tell us how the part is used — the DFM review includes a material recommendation. For a fuller comparison of grades, see our material notes.
Tolerances
We machine to ISO 2768-mK as the default standard when a drawing has no general tolerance block. Quoted tolerance levels:
Level | Metal tolerance | In inches |
|---|---|---|
Standard | ±0.13 mm | ±0.005 in |
Precision | ±0.025 mm | ±0.001 in |
Precision tolerances are applied where you mark them — bearing seats, mating faces, press fits and sealing surfaces. Holding ±0.025 mm across an entire part is possible on request but rarely worth its cost; our DFM review will show you exactly which dimensions we propose to hold tight and which to leave standard, before you commit. Read more in our guide CNC Machining Tolerances Explained: Standard vs. Precision.
Surface Finishes for Aluminum Parts
- As-machined — visible tool marks, lowest cost, right for internal parts
- Bead blasting — uniform matte finish that hides tool marks before coating or anodizing
- Anodizing — clear or colored, for corrosion protection and appearance
- Hardcoat (hard anodizing) — thicker, wear-resistant anodic layer for sliding or outdoor parts
- Polishing and brushing — for visible, cosmetic surfaces
- Painting and powder coating — color-matched protective finishes
- Plating — nickel, chrome or zinc, plus electroless nickel for even coverage on complex shapes
- Black oxide and passivation — available where specified for metal parts in the same order
Tell us the finish on your drawing or in your RFQ; the DFM review will flag any finish that changes critical dimensions (anodizing and plating build up thickness, and we machine with that allowance in mind).
Specifications
Item | Value |
|---|---|
Processes | 3/4/5-axis milling, turning, mill-turn, wire EDM, EDM, drilling & tapping |
Materials | Aluminum 6061 / 7075 / 6063 / 6082 (other metals and plastics available — see below) |
Standard tolerance | ±0.13 mm (±0.005 in), ISO 2768-mK |
Precision tolerance | ±0.025 mm (±0.001 in) on marked dimensions |
Max part size | Up to 800 mm (31.5 in) CNC travel |
MOQ | 1 piece |
Inspection | CMM, dimensional and material reports available; FAI on request |
Lead time | Depends on part size, quantity and finish — confirmed in your quote; expedited production available on request |
Shipping terms | DDP, EXW or FOB; payment by T/T |
Machining other materials too? We also machine stainless steel 303/304/316 Stainless Steel CNC Turned & Milled Parts, carbon and alloy steels, brass, copper, titanium and magnesium, plus engineering plastics including ABS, POM, PC, PA, PEEK, PTFE and UHMW.
Quality and Inspection
HAFO Mould is ISO 9001:2015 certified (scope: Manufacturing of Hardware Molds and Parts). Aluminum parts are inspected against your drawing before packing, and our metrology lab runs 3 fully automatic CMMs. Available with your order on request:
- CMM inspection report
- Dimensional inspection report
- Material certificate
- Surface finish certificate
- First Article Inspection (FAI) report
- Pre-shipment photos or video of your actual parts
If a dimension matters to your assembly, mark it on the drawing — it will be measured and reported, not just machined.
How Ordering Works
- Send your files. Upload your STEP/IGES file or 2D drawing and tell us material, quantity and finish. NDAs are welcome — ask and we sign before you share anything sensitive.
- Free DFM + quote within 24 hours. An engineer reviews manufacturability, suggests cost-saving changes, and we quote with tolerances and lead time confirmed in writing.
- Production. Your parts are machined in our Dongguan factory; progress photos or video available on request.
- Inspection and reports. Parts are checked against the drawing; reports listed above are supplied when requested.
- Shipping. Packed and shipped on DDP, EXW or FOB terms — we regularly deliver worldwide. Payment by T/T.
Why Buyers Order Aluminum Parts from HAFO
- Factory-direct, no middleman. You talk to the factory that machines your parts — no platform markup and no order passed down a chain of workshops.
- An engineer reviews every RFQ. DFM feedback comes from the people who will run the job.
- Machining, tooling and molding under one roof. When your aluminum prototype grows into a molded product, the same factory builds the tool Custom Plastic Injection Molds and runs production Custom Injection Molded Parts — no second supplier to qualify.
- Small batches treated seriously. A 1-piece prototype gets the same DFM review and inspection as a production run.
Applications
Robotics and automation components, electronics enclosures, drone and UAV frames, bicycle and sports components, optical and instrument housings, automotive brackets and fixtures, consumer product hardware. See where our parts are used: Industrial Equipment & Robotics and Electronics & Enclosures.
Design Tips That Lower Your Aluminum Machining Cost
These are the changes our engineers suggest most often in DFM reviews — none of them alter how your part works, all of them reduce what it costs:
- Give internal corners a radius. A rotating cutter cannot make a sharp internal corner. Specifying a corner radius that matches a standard tool size removes EDM or special-tool operations from the quote.
- Keep walls machinable. Very thin walls deflect under the cutter and force slow, careful passes. A small increase in wall thickness — where your design allows it — often pays for itself in machine time.
- Watch deep, narrow pockets and holes. Depth many times the tool diameter means special tooling and slower feeds. Splitting a deep feature into a through-feature plus a cover plate is sometimes the cheaper architecture.
- Tolerance the interfaces, not the silhouette. Bearing seats, mating faces and sealing surfaces deserve precision callouts; outer profiles rarely do. Our tolerance guide explains the logic in full CNC Machining Tolerances Explained: Standard vs. Precision.
- Remember that finishes add thickness. Anodizing and plating build measurable material on every surface. Tell us the finish at RFQ stage and we machine critical dimensions with the build-up allowed for, instead of correcting parts afterwards.
- Consolidate setups. Features machinable from fewer directions cost less and locate more accurately to each other. If your part can be re-oriented so the important features share one setup, the quote will show it.
None of this requires a redesign meeting: send the file, and the DFM review returns these notes with the quote, within 24 hours, free.
FAQ
What aluminum grades do you machine?
6061, 7075, 6063 and 6082 are our standard grades. 6061 suits most parts; 7075 is the high-strength option; 6063 gives the best anodizing appearance; 6082 is common on European structural drawings. If your drawing specifies another grade, send it — we will confirm availability in the DFM review.
What tolerances can you hold on aluminum?
Standard is ±0.13 mm (±0.005 in) under ISO 2768-mK. Precision dimensions can be held to ±0.025 mm (±0.001 in) where marked. We recommend tolerancing only the features that need it — the free DFM review identifies them with you.
What is the largest aluminum part you can machine?
Our maximum CNC travel is 800 mm (31.5 in). Most enclosures, plates and housings fall well inside that. Parts larger than 800 mm in one dimension — send the file anyway; we will tell you honestly in the DFM review whether and how it can be done.
Is there a minimum order quantity?
No. MOQ is 1 piece. Prototypes and small batches are a normal part of our work, and the per-part price simply reflects the setup time shared across your quantity.
Can you anodize the parts, or do I need a separate finisher?
We supply anodizing (including hardcoat), bead blasting, polishing, brushing, painting, powder coating and plating as part of the same order. One supplier is accountable for the finished part, dimensions included.
How fast will I get a quote?
Within 24 hours of receiving your files. The quote follows a free engineering DFM review, and it confirms material, tolerance approach, finish and lead time in writing.
How long is production lead time?
It depends on part size, quantity and finish, so we confirm it in the quote rather than publishing a generic number. If you have a hard deadline, tell us — expedited production is available on request.
What inspection reports can I get?
CMM reports, dimensional reports, material certificates, finish certificates and FAI reports are available on request, plus pre-shipment photos or video of your parts before they leave.
Can you sign an NDA?
Yes. NDAs are welcome, and every file we receive is treated as confidential whether or not one is signed.
What file formats do you accept?
STEP, STP, IGES, STL and X_T 3D files, or 2D drawings in PDF. A 3D file plus a 2D drawing with tolerances marked is the fastest combination to quote.
What are your payment and shipping terms?
Payment by T/T. We ship on DDP, EXW or FOB terms and regularly deliver worldwide.
My part will later become an injection molded product. Can you help with that step too?
Yes — that is one reason buyers choose a factory with both departments. We machine your aluminum prototypes and, when the design is frozen, build the injection mold Custom Plastic Injection Molds and run molding production in-house.
Related guides: How to Get an Accurate CNC Machining Quote · 5-Axis vs 3-Axis CNC Machining: How to Choose · CNC Machining Tolerances Explained
Ready to start? Upload your drawing for a free DFM review and a quote within 24 hours — Get a Quote.