CNC Machining Cost in China: What Drives the Price Per Part (and How to Reduce It)
CNC machining cost in China has no flat rate. Learn the 7 price drivers, tolerance and quantity effects, and how to estimate your part—then get a free DFM review and a quote from HAFO within 24 hours.
The direct answer: There is no honest flat rate for CNC machining in China — no per-kilo or per-hour price list that fits every part. A part's price is built from one equation: unit price ≈ (material + machine time + setup) ÷ quantity + finishing + inspection. The same bracket can cost a fraction of itself, or several times itself, depending on the material grade, the tolerances you specify, how many faces need machining, and how many pieces you order. The fastest way to a real number is not a price list — it is a drawing. Send HAFO a STEP file and a dimensioned drawing and an engineer returns a quote within 24 hours, after a free DFM review. CNC from 1 piece, no tooling to build, no mold to wait for — which is exactly why CNC is the fastest route from a drawing to a part in your hand, and why it is the centre of what HAFO does.
At a glance: CNC machining at HAFO
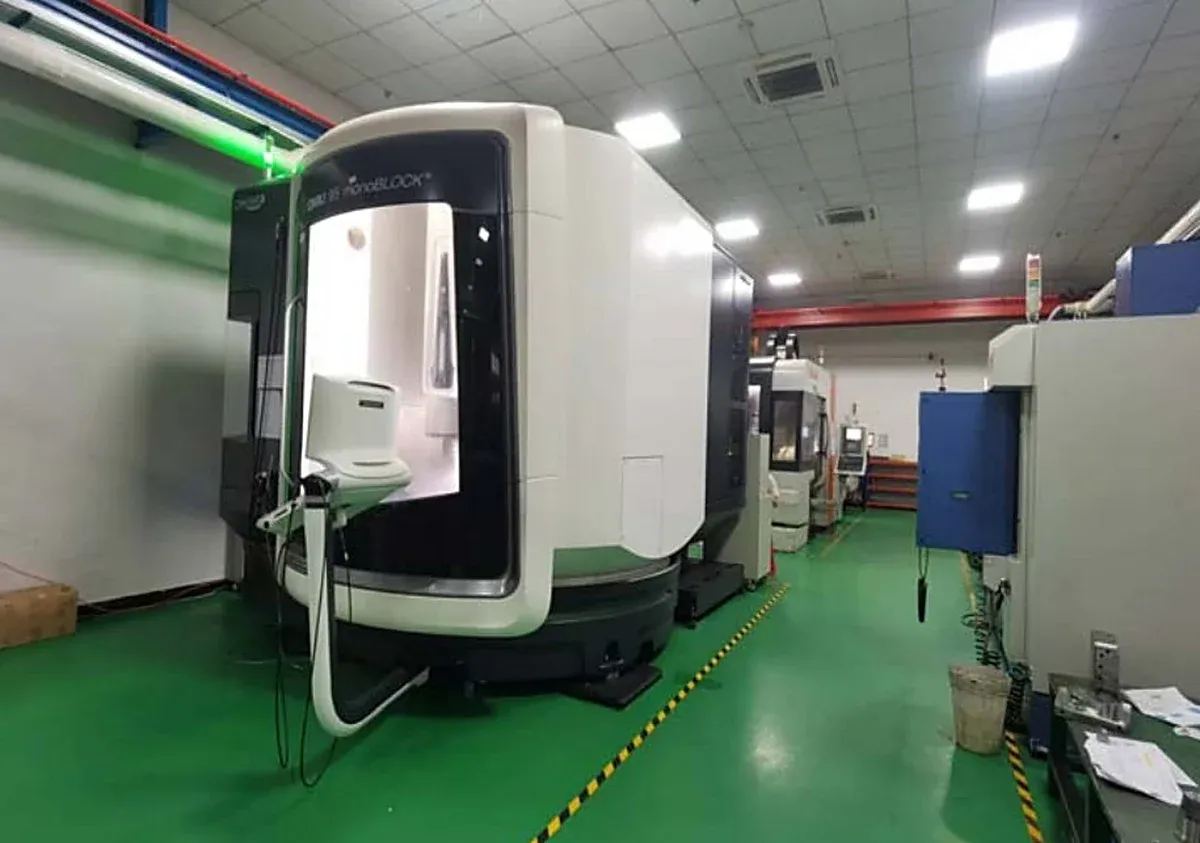
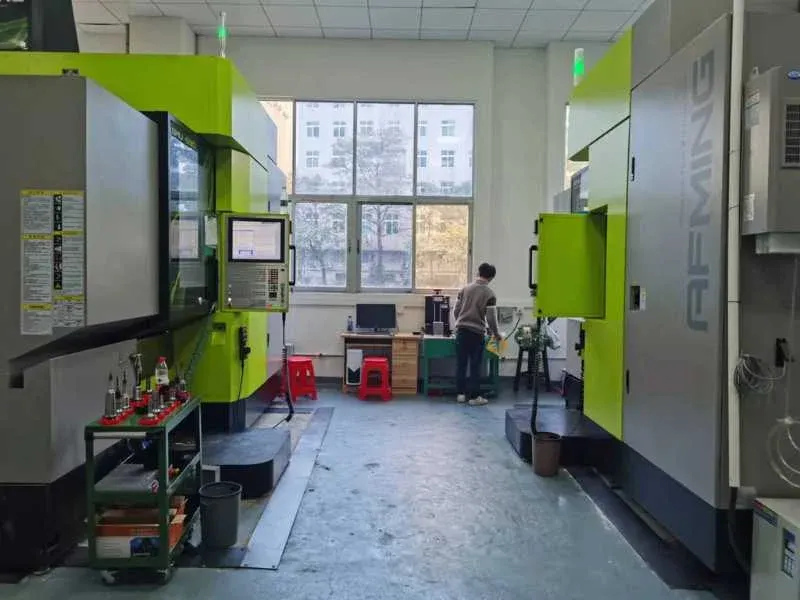
HAFO is a factory in Chang'an, Dongguan, making CNC hardware parts (CNC五金零件加工) since 2007. Machining is not a sideline here — it is the core of the business, with the mold shop, the molding presses and the die-casting finishing all in the same factory, so a machined part, a molded part and a die-cast part can all be finished by CNC under one roof.
| Capability | HAFO (verified) |
|---|---|
| CNC machining centres | 69 — 38× 3-axis, 13× 4-axis, 18× 5-axis |
| Max travel | 800 mm |
| Turning | To Ø500 mm × 1500 mm |
| Toolroom (in-house) | 13 high-speed CNC, 8 EDM, 6 wire-cut |
| Standard tolerance | ISO 2768-mK, ±0.13 mm |
| Precision tolerance | ±0.025 mm on annotated dimensions |
| Aluminium | 6061, 7075, 6063, 6082 |
| Stainless steel | 303, 304, 316 |
| Minimum order | 1 piece |
| Surface treatments | Anodizing (incl. hard), sandblasting, spraying, powder coating, plating, passivation, polishing |
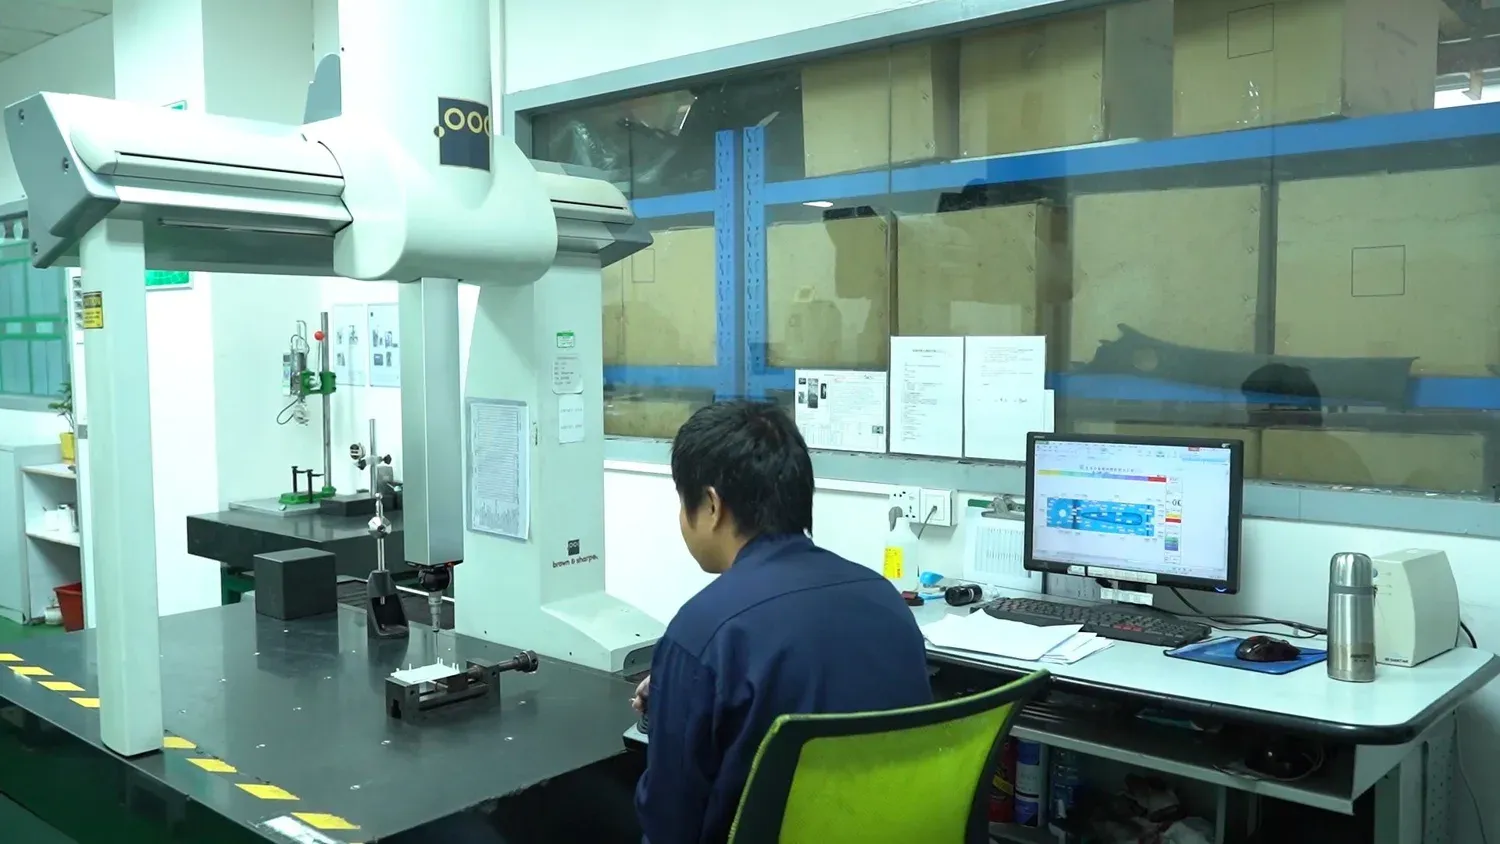
| Inspection | 3 fully automatic CMMs; CMM / dimension / material / surface-treatment / first-article reports on request |
| Quality | ISO 9001:2015, certificate 64625Q02009R000, valid to 26 December 2028 |
| Quote | Free DFM review, quote within 24 hours |
If you are comparing suppliers, that table is the whole story in one place: the machine count and axis mix decide which parts can be made in one setup, the tolerance levels decide what "precision" actually costs, and the 1-piece minimum decides whether a prototype is a real option or a favour. Keep it open while you read the rest of this guide — every driver below maps back to a line in it.
Why CNC closes faster than the alternatives
Buyers close CNC orders faster than mold orders for a simple reason: there is nothing to build first. A mold order starts with tool design, steel, machining, fitting and trials before the first good part exists. A CNC order starts with your file. Programming, a setup, and the part is being cut. That is why CNC is where most new buyer–supplier relationships start, and why HAFO puts it at the centre of the website: a first CNC order is a low-risk way to test a factory's engineering, communication and quality before committing to tooling.
It also changes how you should think about cost. On a molded part, the mold is the cost and the piece price is small. On a machined part, the part is the cost — every minute of machine time, every setup and every tight tolerance is visible in the unit price. That transparency is an advantage: it means you can actually engineer the price down, feature by feature, before you order. This guide shows you how.
How a CNC quote is actually built
Every professional quote — factory or platform — is an estimate of the same equation:
Unit price ≈ (material cost + machine time + setup cost) ÷ quantity + finishing + inspection / documentation
Suppliers differ in how efficiently they execute each term. A factory quoting its own machine time, with no platform margin in between, starts from a different cost base than a marketplace adding a percentage on top of a subcontractor's price. But even between two honest factory quotes, the inputs explain most of the spread: your drawing, your material, your tolerances. Understand each term and you are in control of them.
The rest of this guide takes the equation apart, one term at a time, and then puts it back together as a method you can use on your own drawing.
The 7 cost drivers, and what each one does to your quote
HAFO's existing guide What Does CNC Machining Cost? already explains these seven drivers in depth. This guide adds the numbers that let you weigh them: which drivers are big, which are small, and where the money actually sits.
| # | Driver | What it does | How big is it? |
|---|---|---|---|
| 1 | Material | Stock grade, stock form, how much becomes chips, certification | Often 20–40% of the unit price; the grade alone can multiply stock cost several times |
| 2 | Machine time | Volume removed, feature count, hole/thread depth, sharp internal corners | Usually the largest single term; geometry is money |
| 3 | Setups | Every re-clamp, re-position and re-indication; features across many faces | Each extra setup adds operator time, fixture attention and error risk — and the tightest inter-face tolerances |
| 4 | Tolerances | Slower finishing passes, in-process measurement, more inspection | The single biggest lever after material: precision everywhere can rival the machining itself |
| 5 | Surface finish | Every step after machining: blasting, anodizing, polishing, coating, plating | As-machined is the baseline; a finish chain can rival the machining cost on a small part |
| 6 | Quantity | Programming, fixturing, setup and first-article inspection are fixed per order | The steepest curve in the guide: 1 piece pays all of it, 100 pieces spread it thin |
| 7 | Inspection & documentation | CMM reports, FAI packages, material and finish certificates, photos | Standard inspection is included; evidence level is a line item — cheap next to a rejected shipment |
Read the table as a priority list. If your quote is too high, start at the top and work down: material, machine time, setups, tolerances. Finish and documentation are real costs, but they rarely explain a quote that is twice what you expected. Tolerance and setup choices usually do.
Driver 1: Material — what you buy vs. what you keep
You pay for the stock the part is cut from, not the finished weight. Three things matter: the grade, the stock form, and certification.
Aluminium 6061 is the economy benchmark for machined parts — easy to cut, widely stocked, and the grade most buyers should start from unless a property forces them elsewhere. 7075 is stronger but costs meaningfully more as stock and machines somewhat slower. Stainless steels (303, 304, 316) cost more than aluminium grades as stock, cut slower, wear tools faster, and run longer cycles — the same shape in 304 stainless will always cost more than in 6061, and that is fair, not margin. Engineering plastics span a wide range, with high-performance grades such as PEEK at the expensive extreme.
Stock efficiency is the part buyers most often miss. Cut a part from a thick block where 80% becomes chips and you pay more — in material and in roughing time — than the same part nested efficiently in plate or cut from a near-size extrusion. Deep pockets and tall thin walls are, materially, parts you pay to throw away. If your design can start closer to its stock shape, it machines faster and wastes less.
Certification is a real (if modest) cost line: material certificates with traceability. Ask for them in the RFQ. Asking mid-production is worse than asking up front. HAFO's Materials pages cover the aluminium and stainless grades in detail, and the 6061 vs 7075 guide covers the most common upgrade decision — when 7075 earns its premium, and when it is just a tax.
| Material (HAFO) | Relative stock cost | Machinability | Typical use |
|---|---|---|---|
| Aluminium 6061 | 1.0× (benchmark) | Excellent | General housings, brackets, plates, enclosures |
| Aluminium 6063 | ~1.0× | Excellent | Extruded profiles, trim, heatsink-style parts |
| Aluminium 6082 | ~1.0–1.2× | Very good | Structural parts, higher-strength plates |
| Aluminium 7075 | Meaningfully higher | Good, slower than 6061 | High-strength, aerospace-style, thin-wall load parts |
| Stainless 303 | Higher than aluminium | Good (free-machining) | Shafts, fittings, fasteners, turned parts |
| Stainless 304 | Higher than aluminium | Slower, more tool wear | General corrosion-resistant parts, food/industrial |
| Stainless 316 | Highest of the three | Slowest, most tool wear | Marine, chemical, medical-adjacent environments |
Relative stock costs are illustrative market patterns, not a HAFO price list. Your quote states the actual grade and form.
Driver 2: Machine time — geometry is money
Machine time is usually the largest single term, and your geometry sets it. Volume to remove, feature count and type, part size against the machine, and whether the geometry needs 3, 4 or 5 axes.
Every hole, thread, pocket and contour adds toolpaths. Threads run slower than clearance holes. Deep small-diameter holes run slower than shallow ones. Sharp internal corners force smaller tools and extra passes — or a wire-EDM operation — because a rotating cutter cannot cut a perfectly square inside corner. A small radius that matches a standard end mill removes all of that.
Part size matters against the machine: HAFO's centres go up to 800 mm of travel. A part that fits a standard 3-axis centre costs less than one that needs the largest machine in the shop — and less than one that needs turning to Ø500 mm × 1500 mm. Design close to your stock shape, and the part machines fast.
Driver 3: Setups — the hidden multiplier
A setup is every time the part gets unclamped, repositioned and re-indicated. Each one costs operator time and fixture attention — and hands you a fresh opportunity for error. A part machined complete in one setup is cheaper and more accurate than the same part in three.
- Features scattered across many faces cost more than features on few.
- Tight tolerances between features on different faces cost the most of all. They have to survive repositioning.
- Good DFM often comes down to one question: can this feature move to the same face as the others?
This is also where the axis count earns its keep — see the 3-axis vs 4-axis vs 5-axis table below. Five axes do not exist to make simple parts expensive; they exist to finish a genuinely multi-face part in one setup, which is often cheaper than three setups on a 3-axis machine.
Driver 4: Tolerances — precision is bought by the dimension
Holding a tolerance costs time: slower finishing passes, in-process measurement, sometimes a separate precision operation, always more inspection. Under ISO 2768-mK HAFO quotes two levels — standard (±0.13 mm) and precision (±0.025 mm on annotated dimensions) — and the gap between "precision where it matters" and "precision everywhere" is one of the largest levers in any quote.
| Tolerance callout | What it costs you | When to use it |
|---|---|---|
| ISO 2768-mK standard, ±0.13 mm | Baseline — normal machining and inspection | Clearance faces, cosmetic surfaces, non-mating dimensions |
| Precision ±0.025 mm on one or two features | Slower finishing + measurement on those features only | Bearing seats, press fits, sealing and mating faces |
| Precision ±0.025 mm on every dimension | Slower passes and more inspection on the whole part — can rival the machining cost itself | Almost never justified; the classic budget mistake |
| Tighter than ±0.025 mm | Separate precision operation, dedicated measurement, higher scrap risk — confirm in the quote | Only where the function genuinely demands it |
Effects are relative and illustrative, based on the patterns reported across the synthesised guides — not a HAFO price list. HAFO's DFM review marks which dimensions genuinely need the tight callout and which can relax.
The waste pattern HAFO's engineers see weekly is a blanket precision tolerance in the title block, applied to clearance faces, cosmetic surfaces and non-mating dimensions that would function identically at standard. Buyers are often surprised how much of their quote is tolerance they never needed. Full background is in HAFO's CNC Machining Tolerances Explained guide — read it before you sign off a drawing.
Driver 5: Surface finish — every step after machining adds a step
As-machined is the baseline. Every finish after that is a process — handling, time, yield risk:
| Finish (HAFO) | Cost character | Rule of thumb |
|---|---|---|
| As-machined | Baseline | Leave hidden and non-functional faces here |
| Sandblasting / bead blasting | Light cost, big cosmetic improvement | The standard pre-treatment before anodizing or coating |
| Anodizing / hard anodizing | Real process chain (clean, rack, bath, seal), priced by batch as much as by part | Batch parts together; finish only the faces the world sees |
| Polishing / brushing | Hand-influenced; the smoother you spec it, the slower it goes | A mirror finish on a hidden face is pure waste |
| Spraying / powder coating | Masking threads and precision faces adds labour on top of the coating | Mask only what must stay bare |
| Plating, passivation | Each a separate line in the quote | Cheap insurance on steel and stainless where the environment calls for it; ornament where it does not |
Same rule as tolerances: finish the faces the world sees and the function needs. Leave the rest as-machined.
Driver 6: Quantity — the steepest curve in the guide
Machining carries real fixed costs per order: programming, fixturing, first-article inspection, the setup itself. Spread over one piece, those fixed costs are the price. Over ten pieces they are a tenth as much per part. Over a hundred, cycle time dominates and unit prices fall toward material + machine time.
| Quantity (same part, indexed: 1 pc = 100) | What dominates the unit price | Indexed unit price |
|---|---|---|
| 1 piece (prototype) | Setup, programming, first-article inspection | 100 |
| 10 pieces | Setup still visible; cycle time rising | ~35–55 |
| 100 pieces | Cycle time dominates; setup spread thin | ~15–25 |
| 1,000 pieces | Material + machine time; finish and inspection per part | ~10–15 |
Indexed and illustrative — the shape of the curve is the lesson, not the numbers. The exact curve depends on your part: a simple part flattens fast, a complex part flattens slowly. HAFO quotes from 1 piece, and a one-off will never carry the unit price of a batch — that is arithmetic, not margin.
Two traps. Ordering production quantities of an unproven design — the saving is real money spent on the wrong part. And re-ordering prototypes one at a time after the design has frozen: you pay the setup every single time. Prove the design at prototype quantity, then order in batches that amortise setup. If volume is heading toward the thousands, read CNC Machining vs Injection Molding before ordering more machined parts — at some volume, a mold becomes cheaper per part, and HAFO builds the mold in the same factory.
Driver 7: Inspection and documentation
Standard inspection is included in any professional quote. What adds cost is the level of evidence: CMM reports on defined dimensions, full dimensional reports, first-article inspection (FAI) packages, material and finish certificates, pre-shipment photo confirmation. HAFO can supply all of them — inspection runs on three fully automatic CMMs under the ISO 9001:2015 system — and they are cheap next to a rejected shipment. The expensive version is discovering at delivery that your customer's incoming inspection needed a document nobody produced. Ask for the documentation in the RFQ, where it costs a line item. Not in a dispute, where it costs a relationship.
3-axis vs 4-axis vs 5-axis: which route, and what it costs
Buyers often ask for 5-axis as if it were a quality grade. It is not — it is a route, and the cheapest route is the simplest sufficient route. HAFO runs 38 three-axis, 13 four-axis and 18 five-axis centres, and the DFM review assigns the simplest machine that can make your part correctly.
| Route | Best for | Setup count | Cost character |
|---|---|---|---|
| 3-axis | Features on one or two faces; flat parts, plates, simple housings | 1–2 setups | Cheapest per hour; the right choice for most parts |
| 4-axis | Features around a rotation axis; shafts, fittings, parts with radial holes | 1–2 setups, indexed rotation | Mid-range; removes re-clamping around the axis |
| 5-axis | Angled, curved or multi-face geometry; impellers, complex housings, contoured parts | Often 1 setup | Higher hourly rate, but can be cheaper in total than three 3-axis setups — and more accurate |
The rule: if your part is genuinely multi-face, one 5-axis setup can be cheaper than three 3-axis setups. If your part is flat, 5-axis buys nothing. Force a part onto the wrong machine and it does not get cheaper — it gets extra setups, worse accuracy and a longer total cycle. Ask the supplier which route they plan to use and why; HAFO's quote states the process route, including the axis count.
Estimate it yourself in 4 steps
You do not need a spreadsheet to predict your part's price — you need four honest answers. This is the method the best cost guides converge on, adapted to HAFO's quoting.
Step 1 — Price the material you throw away, not the part you keep. Take the stock size your part must be cut from, not the finished weight. A part cut from a thick block where most of it becomes chips will cost more in material and in roughing time than the same part cut from near-size stock. If the stock is 7075 or 316, note the grade premium; if it is 6061, that is your benchmark.
Step 2 — Count the machine time your geometry needs. Count the features, not the faces: every pocket, hole, thread and contour is toolpath time. Deep pockets, tall thin walls and sharp internal corners are the expensive ones. Then count the faces: features on one or two faces are cheap 3-axis work; features on five faces need rotation or 5-axis, and that is where setups multiply.
Step 3 — Count the setups, then the tight tolerances. One setup is the cheapest setup. Every re-clamp adds cost and risk — and tight tolerances between faces on different setups cost the most of all. Then count how many dimensions are called out at ±0.025 mm, and ask of each one: does the function need it, or did the title block apply it to everything? Precision where it matters is affordable; precision everywhere rarely is.
Step 4 — Add finish and evidence, then divide by quantity. Finish only the faces the world sees. Add the inspection documents your customer actually requires — CMM report, material certificate, first-article package — and nothing more. Then divide the fixed costs (programming, fixturing, setup, first-article inspection) by your quantity. At 1 piece they dominate; at 100 pieces they nearly disappear.
Worked example — the same bracket, four ways (illustrative, indexed)
Same bracket, quoted four ways. No prices here — deliberately, because any number invented would mislead you — but the direction and rough weight of each factor is exactly what a real quote would show. Baseline A is set to 100.
| Version | Specification | Indexed unit price | What dominates |
|---|---|---|---|
| A | 6061 aluminium, standard tolerances, as-machined, batch of 100 | 100 | Machine time; the economy benchmark |
| B | Same part, 7075 aluminium | ~115–130 | Higher stock cost and somewhat slower machining |
| C | Same part, 304 stainless, standard tolerances | ~180–250 | Slower cutting, more tool wear, longer cycle |
| D | Same part, 6061, precision tolerance on every dimension + polished + anodized | ~180–260 | The tolerance blanket and the finish chain rival the machining itself |
Version D surprises buyers most. It is "only aluminium" — yet finishes and tolerances can push it past a plainly specified stainless part. The drawing, not the metal, is usually the price. Now run the same exercise on your own part with the 4 steps above, and you will arrive at the quote meeting already knowing where the money is.
Design changes that cut cost fastest
In order of typical impact — the changes HAFO's engineers look for first in a free DFM review:
- Relax tolerances that do not touch function. Keep precision callouts on mating, bearing and sealing features; let the rest ride at ISO 2768 standard. This is the single biggest saving on most drawings.
- Move features onto fewer faces. One setup is the cheapest setup. A boss moved to the same face as the other features can remove a whole setup.
- Add a radius to sharp internal corners. A small radius that matches a standard end mill removes extra passes or an EDM operation.
- Use standard hole and thread sizes. Non-standard threads mean special tooling and slower cycles.
- Question the material upgrade. 7075, 316 and PEEK are excellent — where they are needed. Where they are not, they are a tax. HAFO's DFM review will say so when it is.
- Specify finish by zone, not by blanket. Cosmetic faces get the cosmetic finish; hidden faces stay as-machined.
- Batch sensibly. Prove the design at prototype quantity, then order in batches that amortise setup. Re-ordering one piece at a time after the design has frozen pays the setup every time.
- Design close to stock shape. A part that starts near its finished shape wastes less material and less roughing time than one milled down from a thick block.
None of these changes hurts the part if the function allows them — and that is the point of the DFM review: finding them in your drawing, before they are priced in.
When CNC is the wrong process
CNC is the centre of HAFO's website because it closes fastest — but a good supplier tells you when another process wins. That honesty is part of why buyers come back.
| Situation | Better process | Why |
|---|---|---|
| Thousands of identical plastic parts per month | Injection molding | The mold is the cost; the piece price falls far below machining |
| One complex plastic prototype, no mold yet | CNC machining (plastic) or 3D printing | No tooling; the part exists in days, not weeks |
| Simple, high-volume metal parts with thin walls | Aluminium / zinc die casting, CNC-finished in-house | Casting forms the shape fast; CNC finishes the precision faces |
| A part that is mostly flat with a few holes | 3-axis CNC or laser / sheet metal | The simplest sufficient route is the cheapest route |
If volume is heading toward the thousands, ask HAFO to compare the CNC price against a molded price for the same part — the mold is built in the same factory, trialled on HAFO's own presses, and the comparison is part of the free DFM review. HAFO's injection mold cost guide explains the mold side of that decision, and CNC Machining vs Injection Molding compares the two routes directly.
What to send for a quote — the RFQ checklist
A complete RFQ gets a faster, more accurate quote. An incomplete one gets a quote with assumptions in it — and assumptions are priced.
| Send | Why it matters | Format |
|---|---|---|
| 3D model | Geometry, volume, feature count — the machine-time estimate | STEP / IGES (STEP is ideal) |
| Dimensioned 2D drawing | Tolerances, finish callouts, intent — the drawing gives what the model cannot | PDF with tolerance and finish callouts |
| Material grade | Stock cost and cutting speed | e.g. 6061, 7075, 303, 304, 316 |
| Quantity (+ expected repeat volume) | Setup amortisation; batch pricing | 1 / 10 / 100 / 1,000 — and whether it repeats |
| Tolerances that matter | Which dimensions are precision, and which are standard | Mark the mating / bearing / sealing faces |
| Finish per zone | Which faces are cosmetic, which are functional | As-machined / anodized / polished / coated |
| Inspection & documents needed | CMM report, material certificate, FAI — asked now, not at delivery | List the documents your customer requires |
| Delivery terms | DDP / EXW / FOB — landed cost is not the piece price | State the Incoterm and destination |
| Confidentiality | NDA before file review, if your company requires it | Say so up front; NDAs are welcome |
Send the 3D model plus the drawing. The model gives geometry; the drawing gives intent. Either alone leaves the quoter guessing — and guessing is priced. Files stay confidential, and NDAs are welcome.
What a HAFO quote includes — and how to compare quotes
So you can compare like with like, a HAFO quote states the material grade and form, the process route (including which axis count is planned), the tolerances as proposed after DFM, the finish steps, the inspection and documentation level included, and the shipping terms (DDP, EXW or FOB — payment by T/T). If a feature will be expensive, the quote says which one, why, and what design change would remove the cost. That is the practical difference between a factory quoting its own work and a middleman forwarding a number.
When you compare quotes from different suppliers, ask each one the same four questions: which dimensions are they holding tight, on what machine, what is included in the price, and what did they assume that you did not state? The answers explain almost every price gap. Be suspicious of any supplier who publishes a flat per-kilo or per-hour price list — it cannot be honest for every part. And be suspicious of the cheapest quote that does not say what it left out: a finish, a document, a setup, a tolerance. The quote that explains itself is usually the quote you can trust.
For the full picture of how HAFO works, see Our Factory & Equipment and Quality & Inspection — 69 machining centres, the toolroom, and the three automatic CMMs behind every quote — and the Materials hub for the grades behind the material table above.
FAQ
Why did two suppliers quote such different prices for the same drawing?
Usually one of three reasons: they read the tolerances differently (blanket precision vs. precision where marked), they plan different process routes (more setups, or a bigger machine than needed), or one of them is not a factory and carries a margin. Ask each supplier which dimensions they are holding tight and on what machine — the answers explain the gap.
Can you give me a rough price from just a photo or a description?
A rough range of drivers, yes; a reliable number, no. Price lives in tolerances, material and features that photos do not show. Send a STEP file or a dimensioned drawing and HAFO returns a real quote within 24 hours, free, after a DFM review.
What is the minimum order quantity?
One piece. CNC at HAFO starts at 1 piece — prototypes are how projects start. Be aware that a one-off carries the full setup cost, so its unit price will never match a batch price. Prove the design first, then order in batches.
Does 5-axis machining always cost more?
No. On a genuinely multi-face part, one 5-axis setup can be cheaper than three 3-axis setups — and more accurate. On a simple part, 5-axis buys nothing. The right question is which route your geometry needs; HAFO's DFM review assigns the simplest sufficient process.
Why is my one prototype so expensive compared with the batch price?
Because programming, fixturing, setup and first-article inspection are fixed per order. On one piece you pay all of them; on a hundred, they are spread thin. This is arithmetic, not margin.
How much do tolerances really add?
Enough that they are the first thing HAFO's engineers check. A blanket precision tolerance can rival the entire machining cost of a loosely specified part, because every dimension gets slower passes and more measurement. Precision where it matters is affordable; precision everywhere rarely is.
Is it cheaper if I supply my own material?
Occasionally, and HAFO can work that way — but usually not: HAFO buys common stock at factory volumes, and supplied material still needs inspection and carries a yield question if it machines badly. Ask in the RFQ and HAFO will compare honestly.
What file format gives the most accurate quote?
A 3D model (STEP is ideal) plus a dimensioned 2D drawing with tolerance and finish callouts. The 3D file gives geometry; the drawing gives intent. Either alone leaves the quoter guessing — and guessing is priced.
Get a quote — free DFM review, within 24 hours
Send your drawing and HAFO's engineers will review it, mark the tolerances and features that drive your price, and return a quote within 24 hours — free, from 1 piece, with no tooling to build first. That is the fastest way to find out what your part actually costs, and the fastest way to start an order.
Contact us — [email protected] · WhatsApp +86-13686606116 · Mon–Fri 9:00–18:00. Or browse CNC machined parts to see what HAFO machines every week.
Written by the HAFO Mould engineering team. Last updated: 2026-11-16. Prices in this guide are illustrative/indexed examples, not quotations — your quote is built from your drawing, within 24 hours of a free DFM review.